A bushing job with a tight fit and a busy line
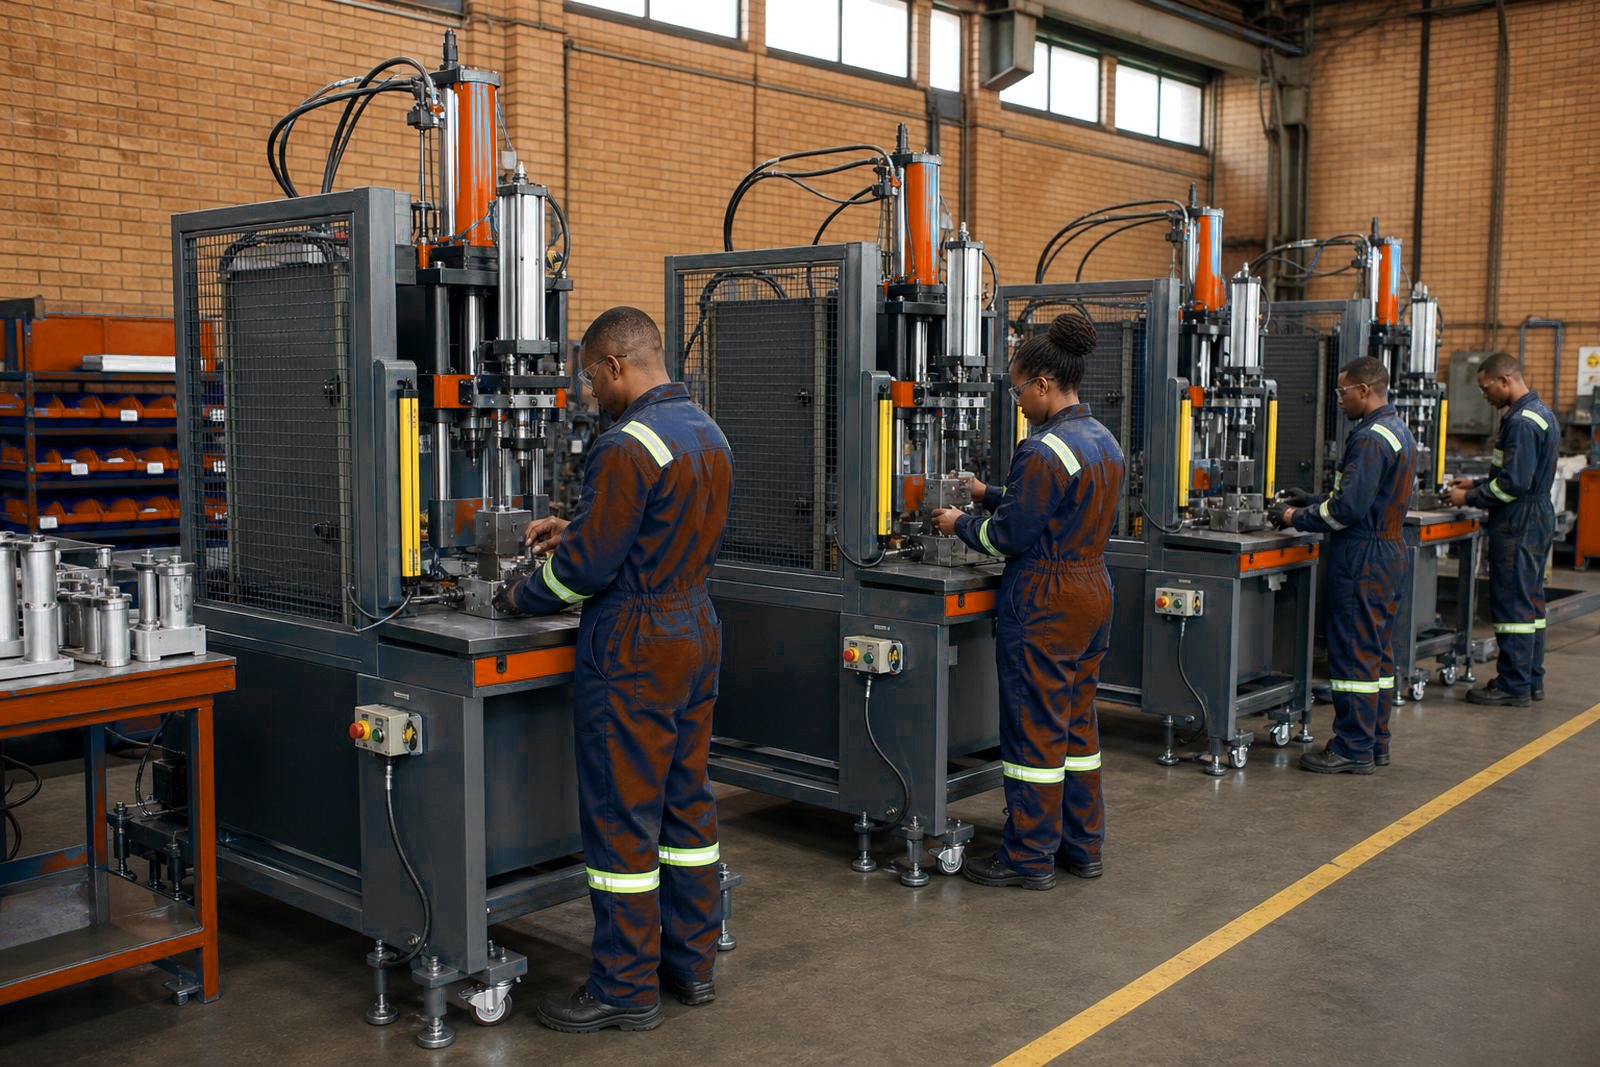
The brief came from a Centurion manufacturer working on a mixed assembly line where bushings had to be inserted into prepared components without bruising the bore or marking the surface. The team wanted a press station that could sit in line with the rest of production, keep the operator in control, and give the same result across a full shift.
Space at the bench was limited, so the machine footprint had to stay practical. The process also needed a guided tool path, because the parts were not forgiving and any side load would show up fast. We planned the station around the part geometry, the insertion depth and the handling method on the floor.
- Job type: bushing insertion for assembly work
- Town: Centurion
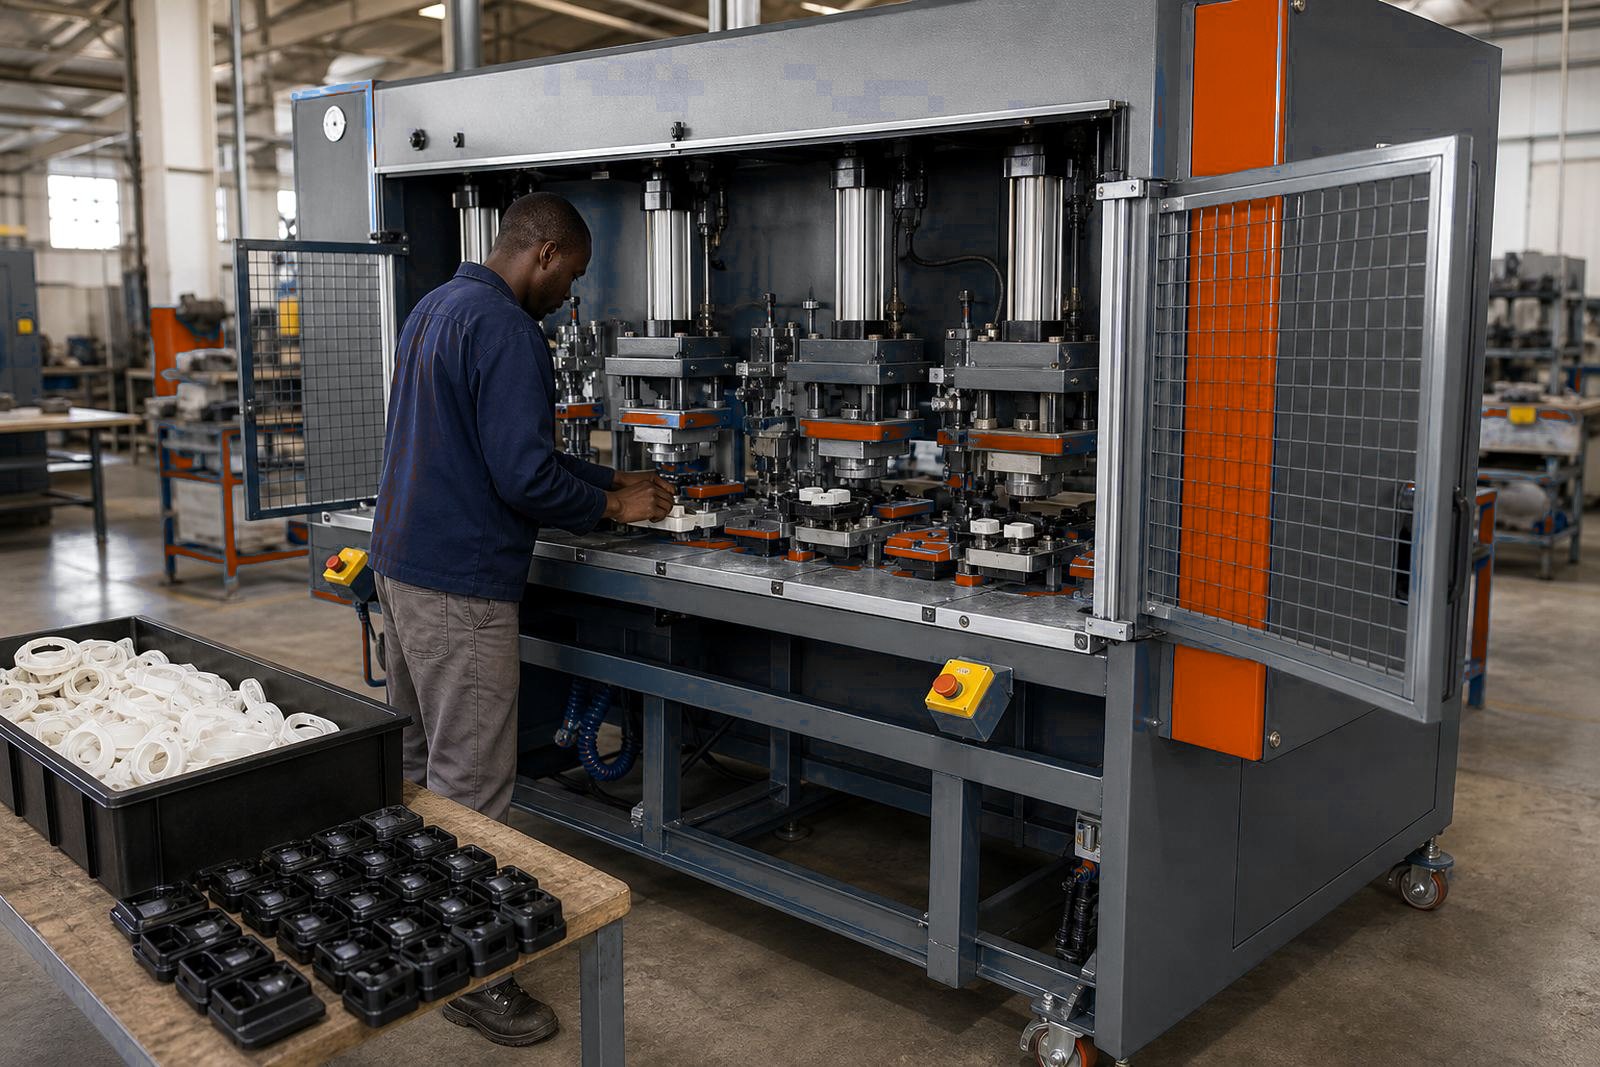
- Press style: multi-station pneumatic press
- Operation: controlled downstroke with guided tooling
Press structure and controls we built in
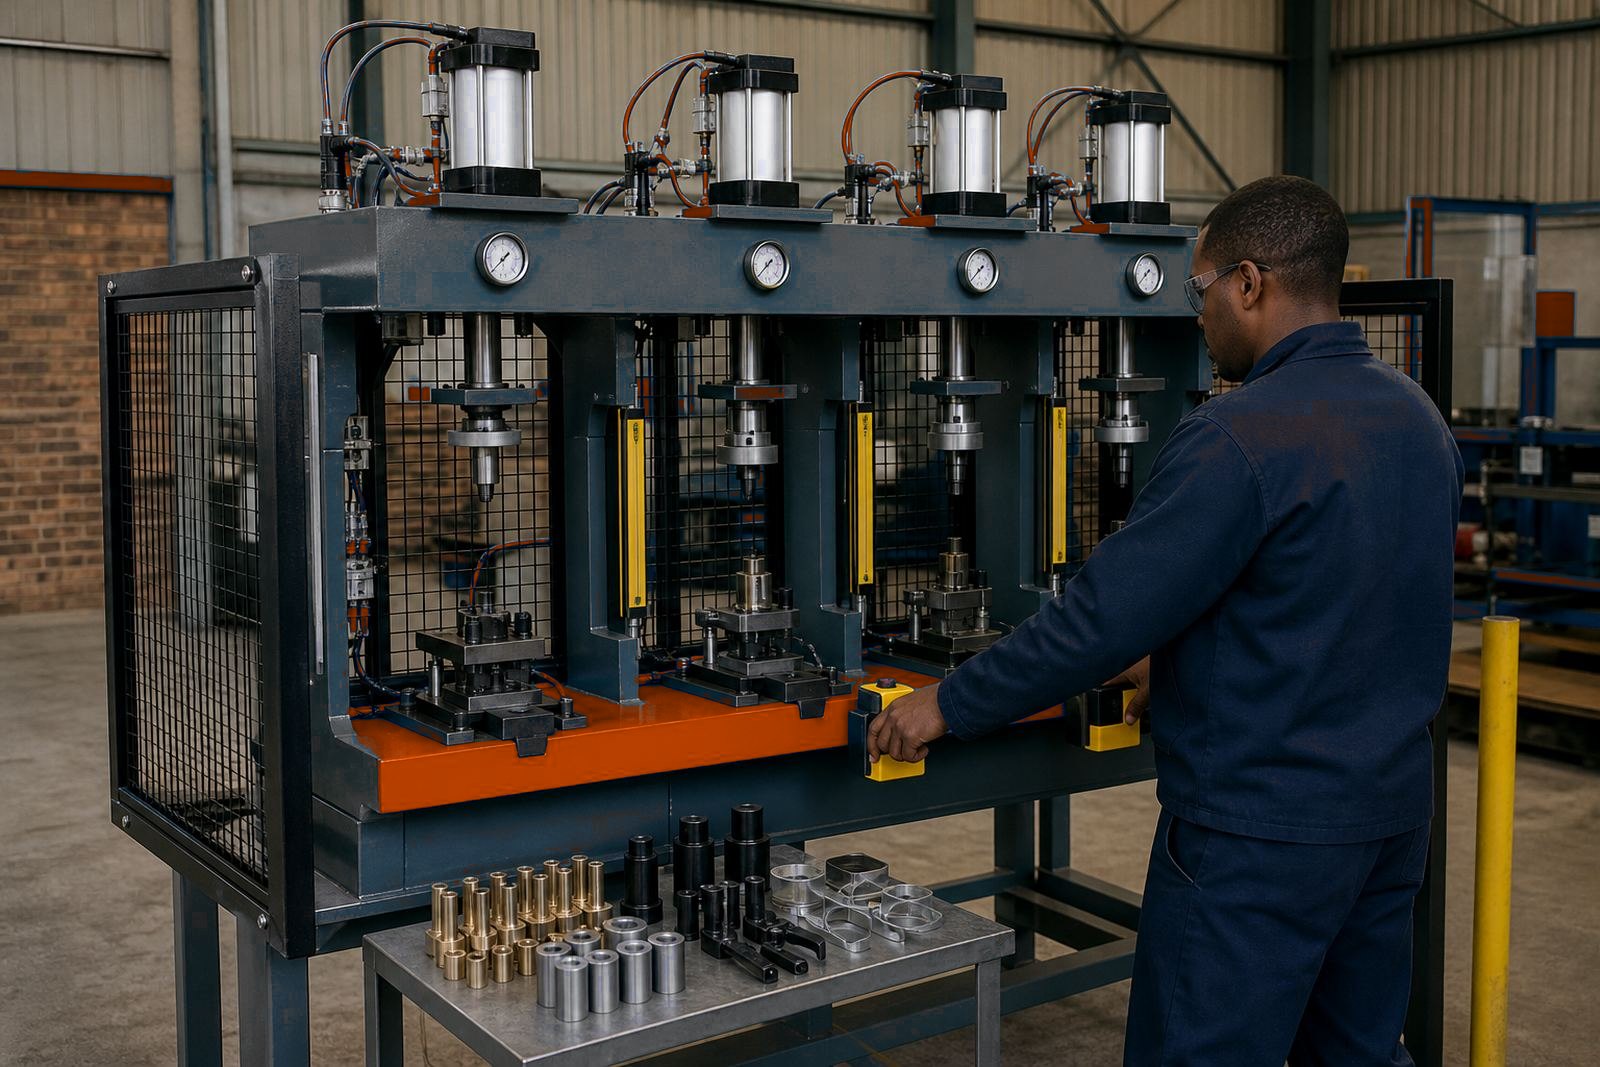
The machine was built around air-driven cylinders sized for the insertion force needed on the job, with stroke setting kept adjustable for the part family. We set the tooling so the bushing starts square, then travels straight into position without wandering. The press frame was arranged for visibility at the working face, which helps the operator watch the part seat properly.
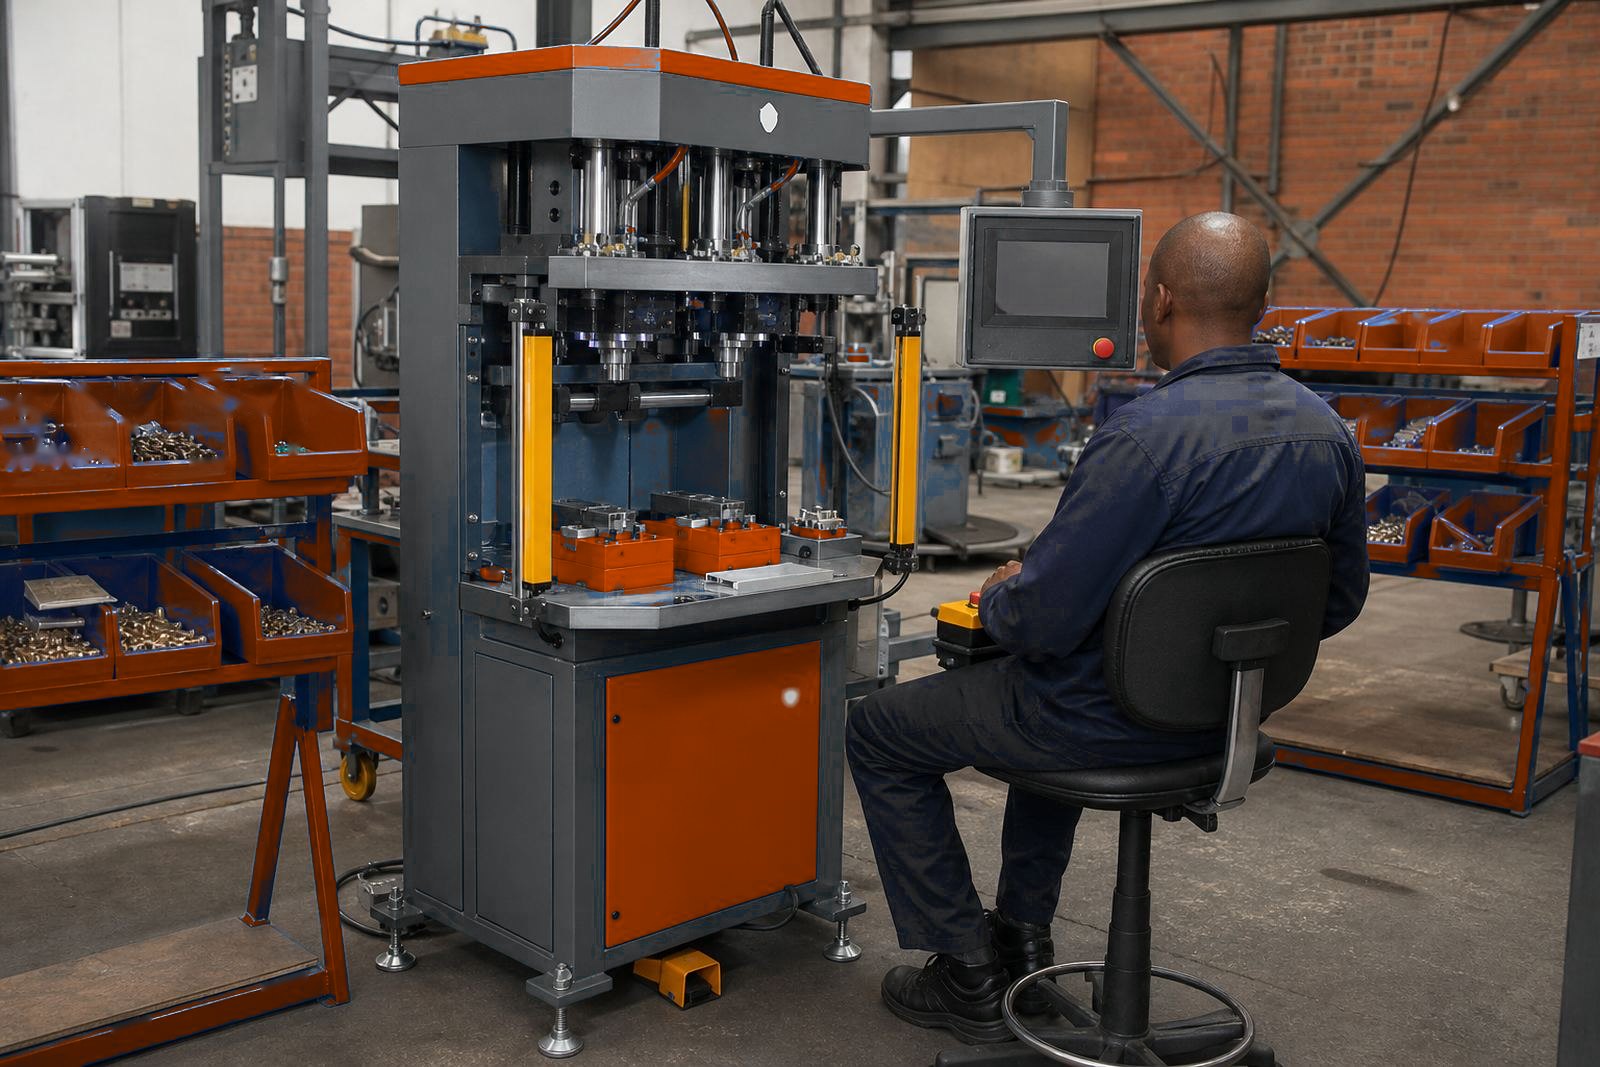
Two-hand controls were included for hand safety and cycle control, and a light curtain was added where the access opening required another layer of protection. The guarding layout allowed loading and unloading without awkward reach, and the station could be used repeatedly without loose movement in the tool path.
- Air actuation with controlled cylinder travel
- Two-hand controls for cycle initiation
- Light curtain protection at the working zone
- Stroke setting matched to the bushing depth
Tooling, fixtures and the insertion path
Musa designed the guided tooling to support the bushing before pressure came on. That mattered because the fit had to stay true under downstroke, and the component could not be asked to self-centre under load. The fixture was shaped for quick location, with a repeatable nest that held the part in the same position every cycle.
The tooling set was made for production wear rather than a one-off demo, and the contact points were designed to be changed without pulling the whole station apart. We also allowed for minor tooling adjustment during setup, because bushing work can shift once a real batch reaches the bench. The final arrangement kept the force where it belonged, on the press axis not on the edges of the part.
- Guided tooling to keep the bushing square
- Dedicated fixture for part location
- Tooling changes handled without major strip-down
- Adjustment points built into the setup
Workshop build, site fit and handover
The frame, guarding and tooling were assembled in our Isando workshop under Johan’s supervision, then checked for fit before site work started. Lerato handled the commissioning on site and verified stroke length, air line setup and basic cycle behaviour once the machine was in place. The installation was completed in three weeks from approval to first production use, with the middle stretch spent on fabrication, fit-up and testing.
We trained operators on correct loading, safe two-hand operation and how to watch for an off-centre bushing before the stroke starts. The handover also covered routine checks on air pressure, tooling condition and guard position, because small changes on a press can affect the job quickly if they are left alone.
- Build and fit-up completed in the workshop
- Commissioning carried out on site
- Operator training included loading and safe cycle control
- Three weeks from approval to handover
What changed on the production floor
Once the press was running, the insertion became more predictable and the team had less variation from one part to the next. The guided stroke reduced the chance of angled starts, which cut down on rework at the bench. The station also helped the line keep its pace because the operator did not need to fight the tool or reposition parts by hand.
For a plant in Gauteng, that kind of control matters when the work is repeated often and the same part comes through many times in a week. The client needed a station that was practical for daily use, not a special machine that only worked under ideal conditions. This one fit the floor routine and stayed within the handling pattern already used on site.
- More even insertion across repeated cycles
- Less rework from angled starts
- Better fit with the existing handling routine
- Cleaner seating of the bushings
What we bring to a comparable press installation
For a job like this, the same first steps would still matter: part measurement, insertion depth, air pressure range, tooling access and the safety layout around the operator’s hands. We would again start with the part in front of us, because bushing work often changes once the first real samples are clamped and pressed.
We would also keep the station simple where possible, then add only the control points that protect the job. That usually means guided tooling, a clear stroke stop, proper guarding and a training session that matches the way the line actually runs. The Centurion installation followed that path and held up well under day to day use.
- Check the part, then set the tooling around it
- Keep the stroke clear and measurable
- Use guarding that suits the access pattern
- Train operators on the exact cycle they will work on
Key facts
| Project | Centurion Bushing Press |
|---|---|
| Town | Centurion, Gauteng |
| Machine type | Multi-station pneumatic press |
| Application | Bushing insertion for assembly |
| Controls | Two-hand controls with light curtain protection |
| Scope | Custom tooling, guarding, commissioning and operator training |